 EN


Engineering guide · Custom CNC gear manufacturing
How to Prepare a Custom CNC Gear RFQ: Design, Backlash, Inspection, and Supplier Selection
A reliable quotation begins with a reliable definition of the part. When a custom gear project starts with a photo, sample, or incomplete CAD model, different suppliers may quote different interpretations of the same component. A clear RFQ turns the request into a shared engineering document.
Before discussing unit price, the buyer should define how the gear must function, how it interfaces with the assembly, and how conformity will be verified. This approach helps engineers, OEM buyers, and procurement teams compare quotations on technical scope rather than on price alone.
What should a custom CNC gear RFQ include?
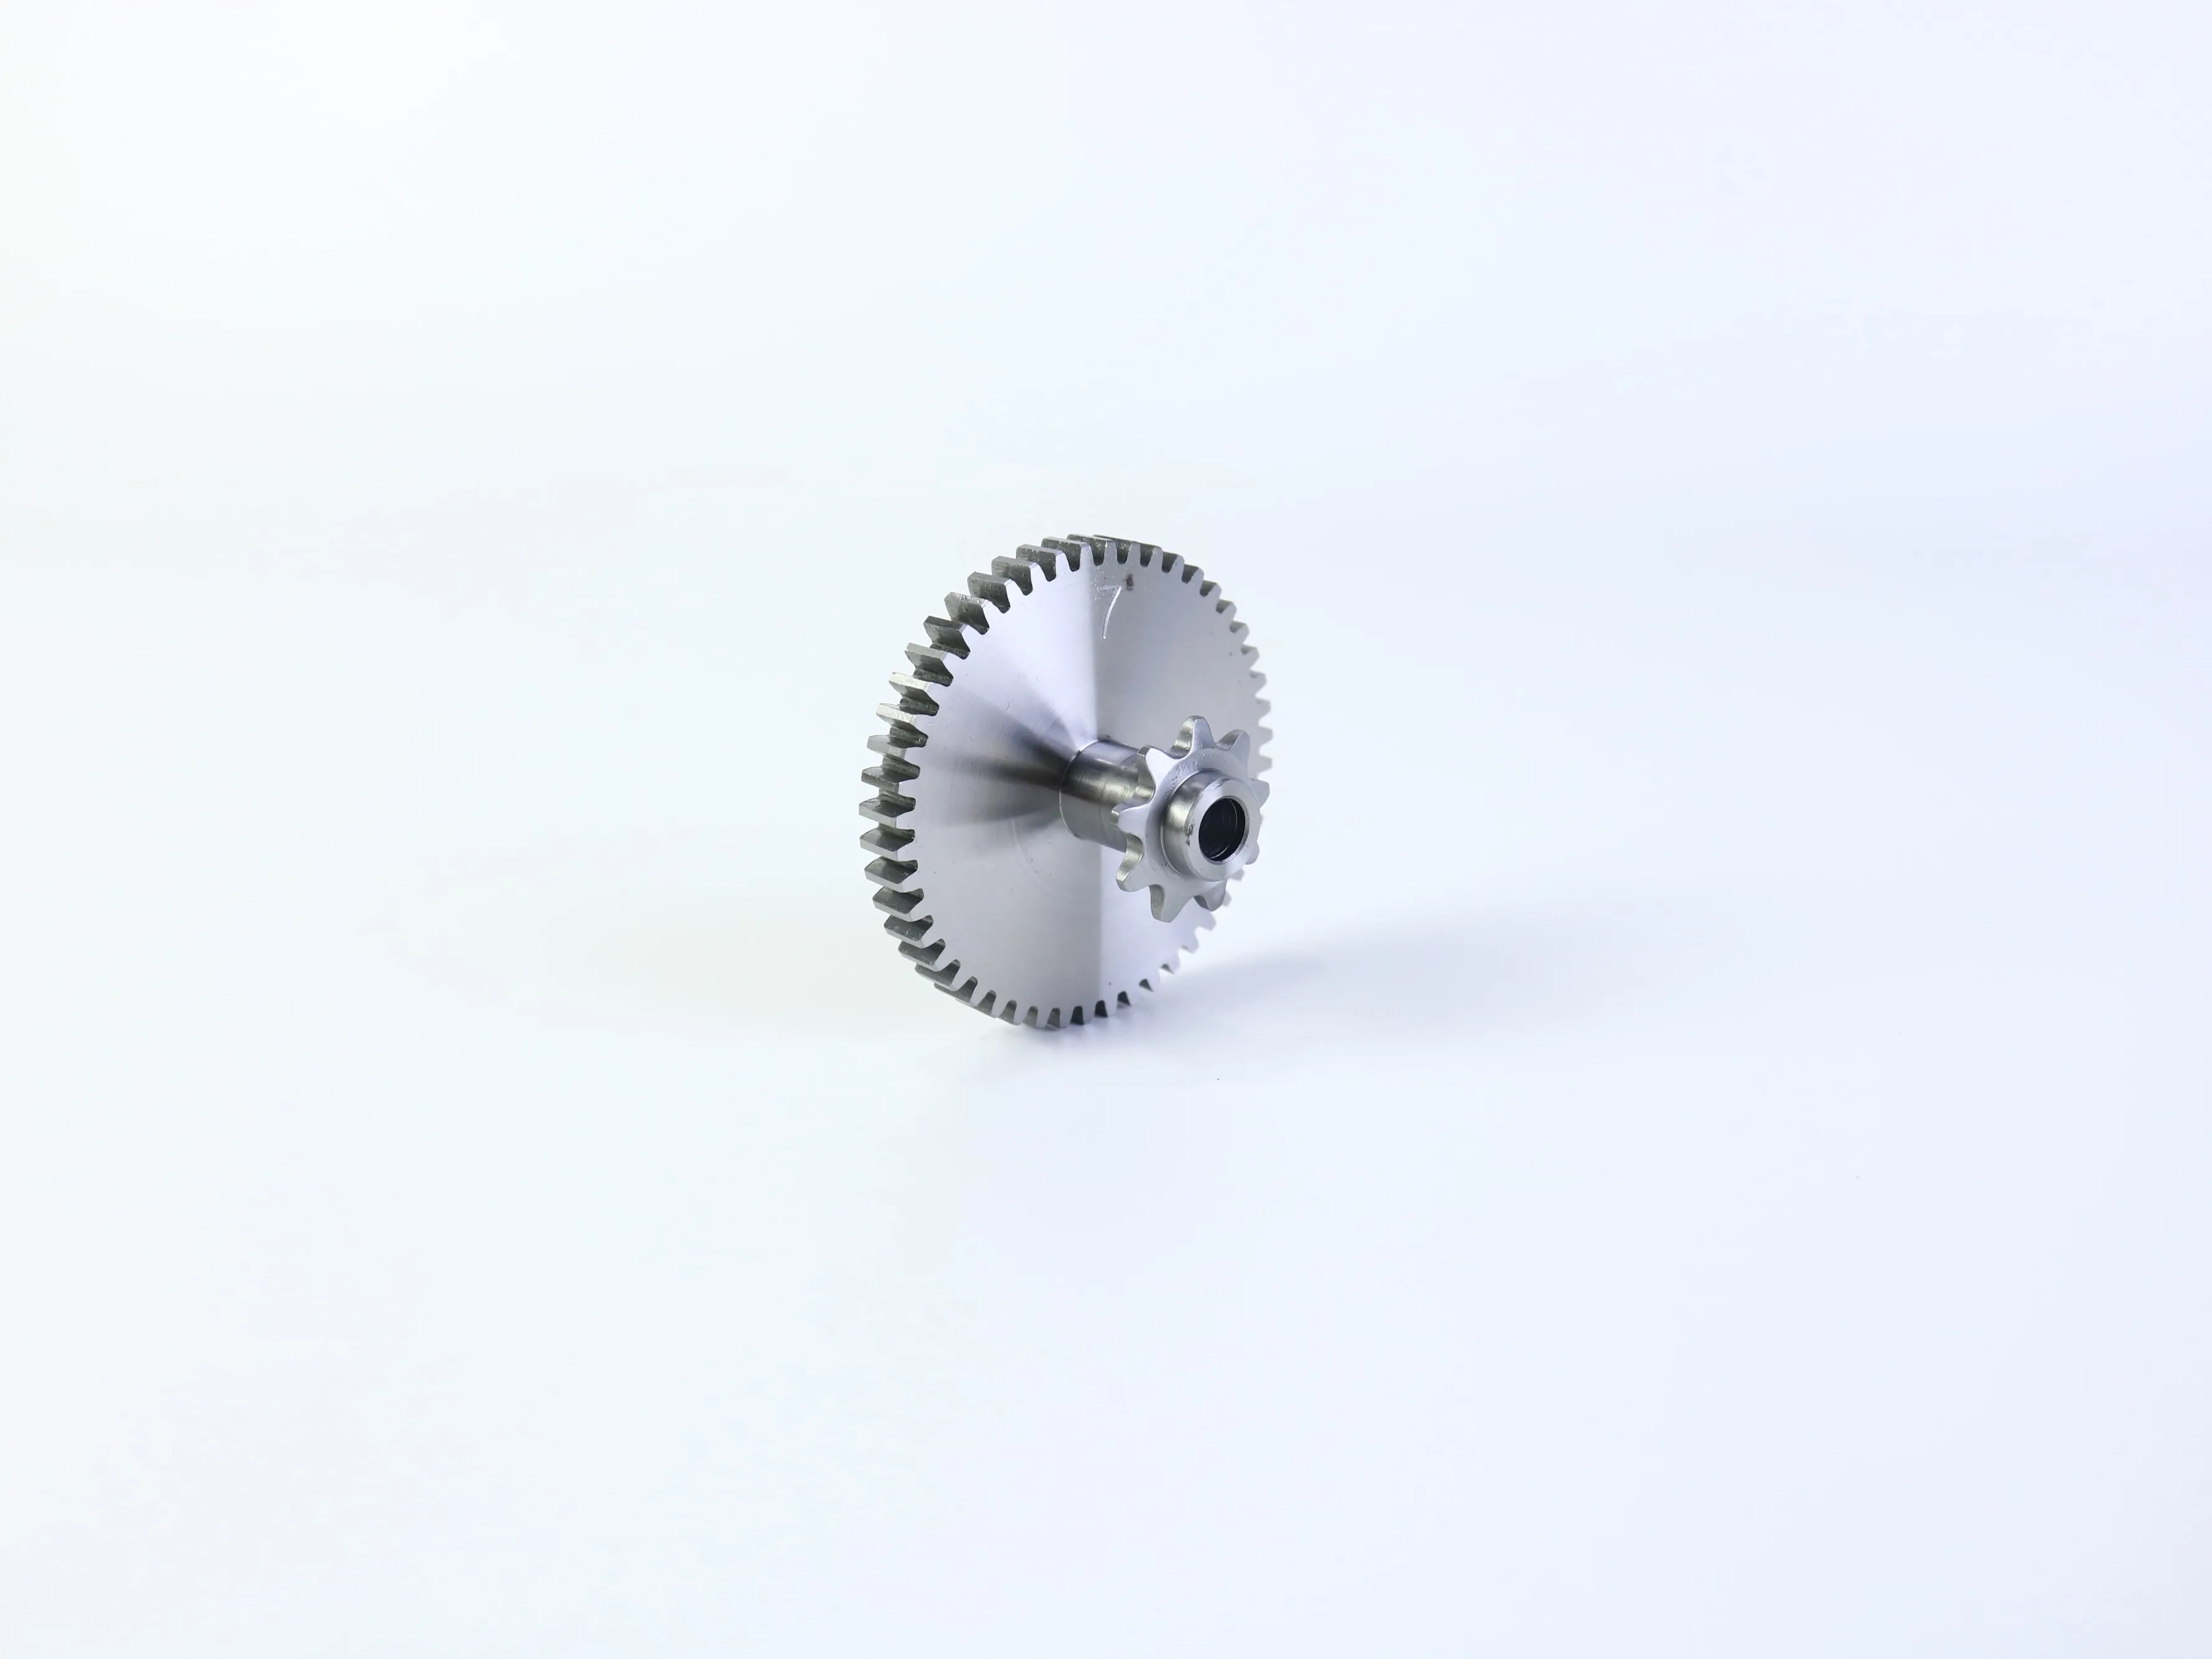
A complete RFQ should provide enough information for suppliers to make the same technical assumptions. Include a revised 2D drawing with datums, dimensions, tolerances, and revision level, together with a 3D CAD model in a commonly supported format. Identify the gear type, tooth form, module or diametral pitch, number of teeth, pressure angle, helix angle where applicable, and hand.
The package should also define the pitch or reference diameter, outside diameter, root information, face width, tooth thickness, bore, keyway, spline, shaft, shoulder, flange, threaded features, material grade, heat treatment, surface finish, deburring, coating, quantity, packaging, and inspection documents. If an item is not known, mark it as TBD instead of allowing every supplier to make a different assumption.
1. Define gear geometry before discussing machining
A gear is not fully defined by its outside appearance or tooth count. For a cylindrical involute gear, module, pressure angle, and number of teeth are fundamental design parameters. Module describes tooth size, pressure angle affects the tooth profile, and tooth count participates in basic dimensional calculations. Two parts can look similar in a photograph and still be incompatible because their tooth systems differ.
If the part is a replacement component, provide the original part number and available wear or failure information, but do not treat the part number as a complete engineering specification. If the gear is integrated with a shaft or hub, clarify whether it is one machined component or an assembly of separate components.
2. Specify backlash as a functional requirement
Backlash is the clearance between mating tooth surfaces. It is not simply a machining defect to eliminate. A controlled amount is generally needed for smooth rotation, lubrication, and allowance for thermal or assembly effects. Backlash can be influenced by center distance and tooth thickness, so the RFQ must describe the complete gear pair rather than quoting an isolated number without context.
The buyer should answer three questions: which gear pair or assembly is being evaluated; which operating condition is relevant, including speed, load, temperature, and lubrication; and how backlash will be measured and accepted. Avoid writing only “zero backlash” unless the engineering team has defined the complete mechanism and adjustment method. Zero clearance can prevent smooth rotation, while a low-backlash requirement without a measurement direction or test condition is difficult to interpret.
If the exact target is not available, request a supplier review and a proposed manufacturable range for approval. That proposal should be documented as an engineering recommendation, not treated as an automatic substitute for the buyer’s functional requirement.
3. Separate critical tolerances from general dimensions
Over-tolerancing every dimension can make a gear RFQ harder to quote and increase machining, setup, and inspection effort without improving the assembly. A better drawing identifies the features that control function. Typical critical areas include tooth flank accuracy or a specified gear accuracy class, the relationship between pitch diameter and mating geometry, bore-to-tooth concentricity, radial and face runout, face width, axial location, keyway or spline fit, shoulder relationships, tooth thickness, backlash, and surface roughness on bearing or sliding interfaces.
ANSI/AGMA ISO 1328-1 provides a classification system for manufacturing and conformity assessment of tooth flanks of individual cylindrical involute gears. It can serve as a common reference, but it does not replace the complete design definition, mating conditions, or acceptance plan. State the standard, edition, and tolerance class required, and confirm whether the supplier can inspect to that reference. Use explicit tolerances and datums for functional dimensions, while a general tolerance may be suitable for non-critical features.
4. Choose the manufacturing route from geometry and quantity
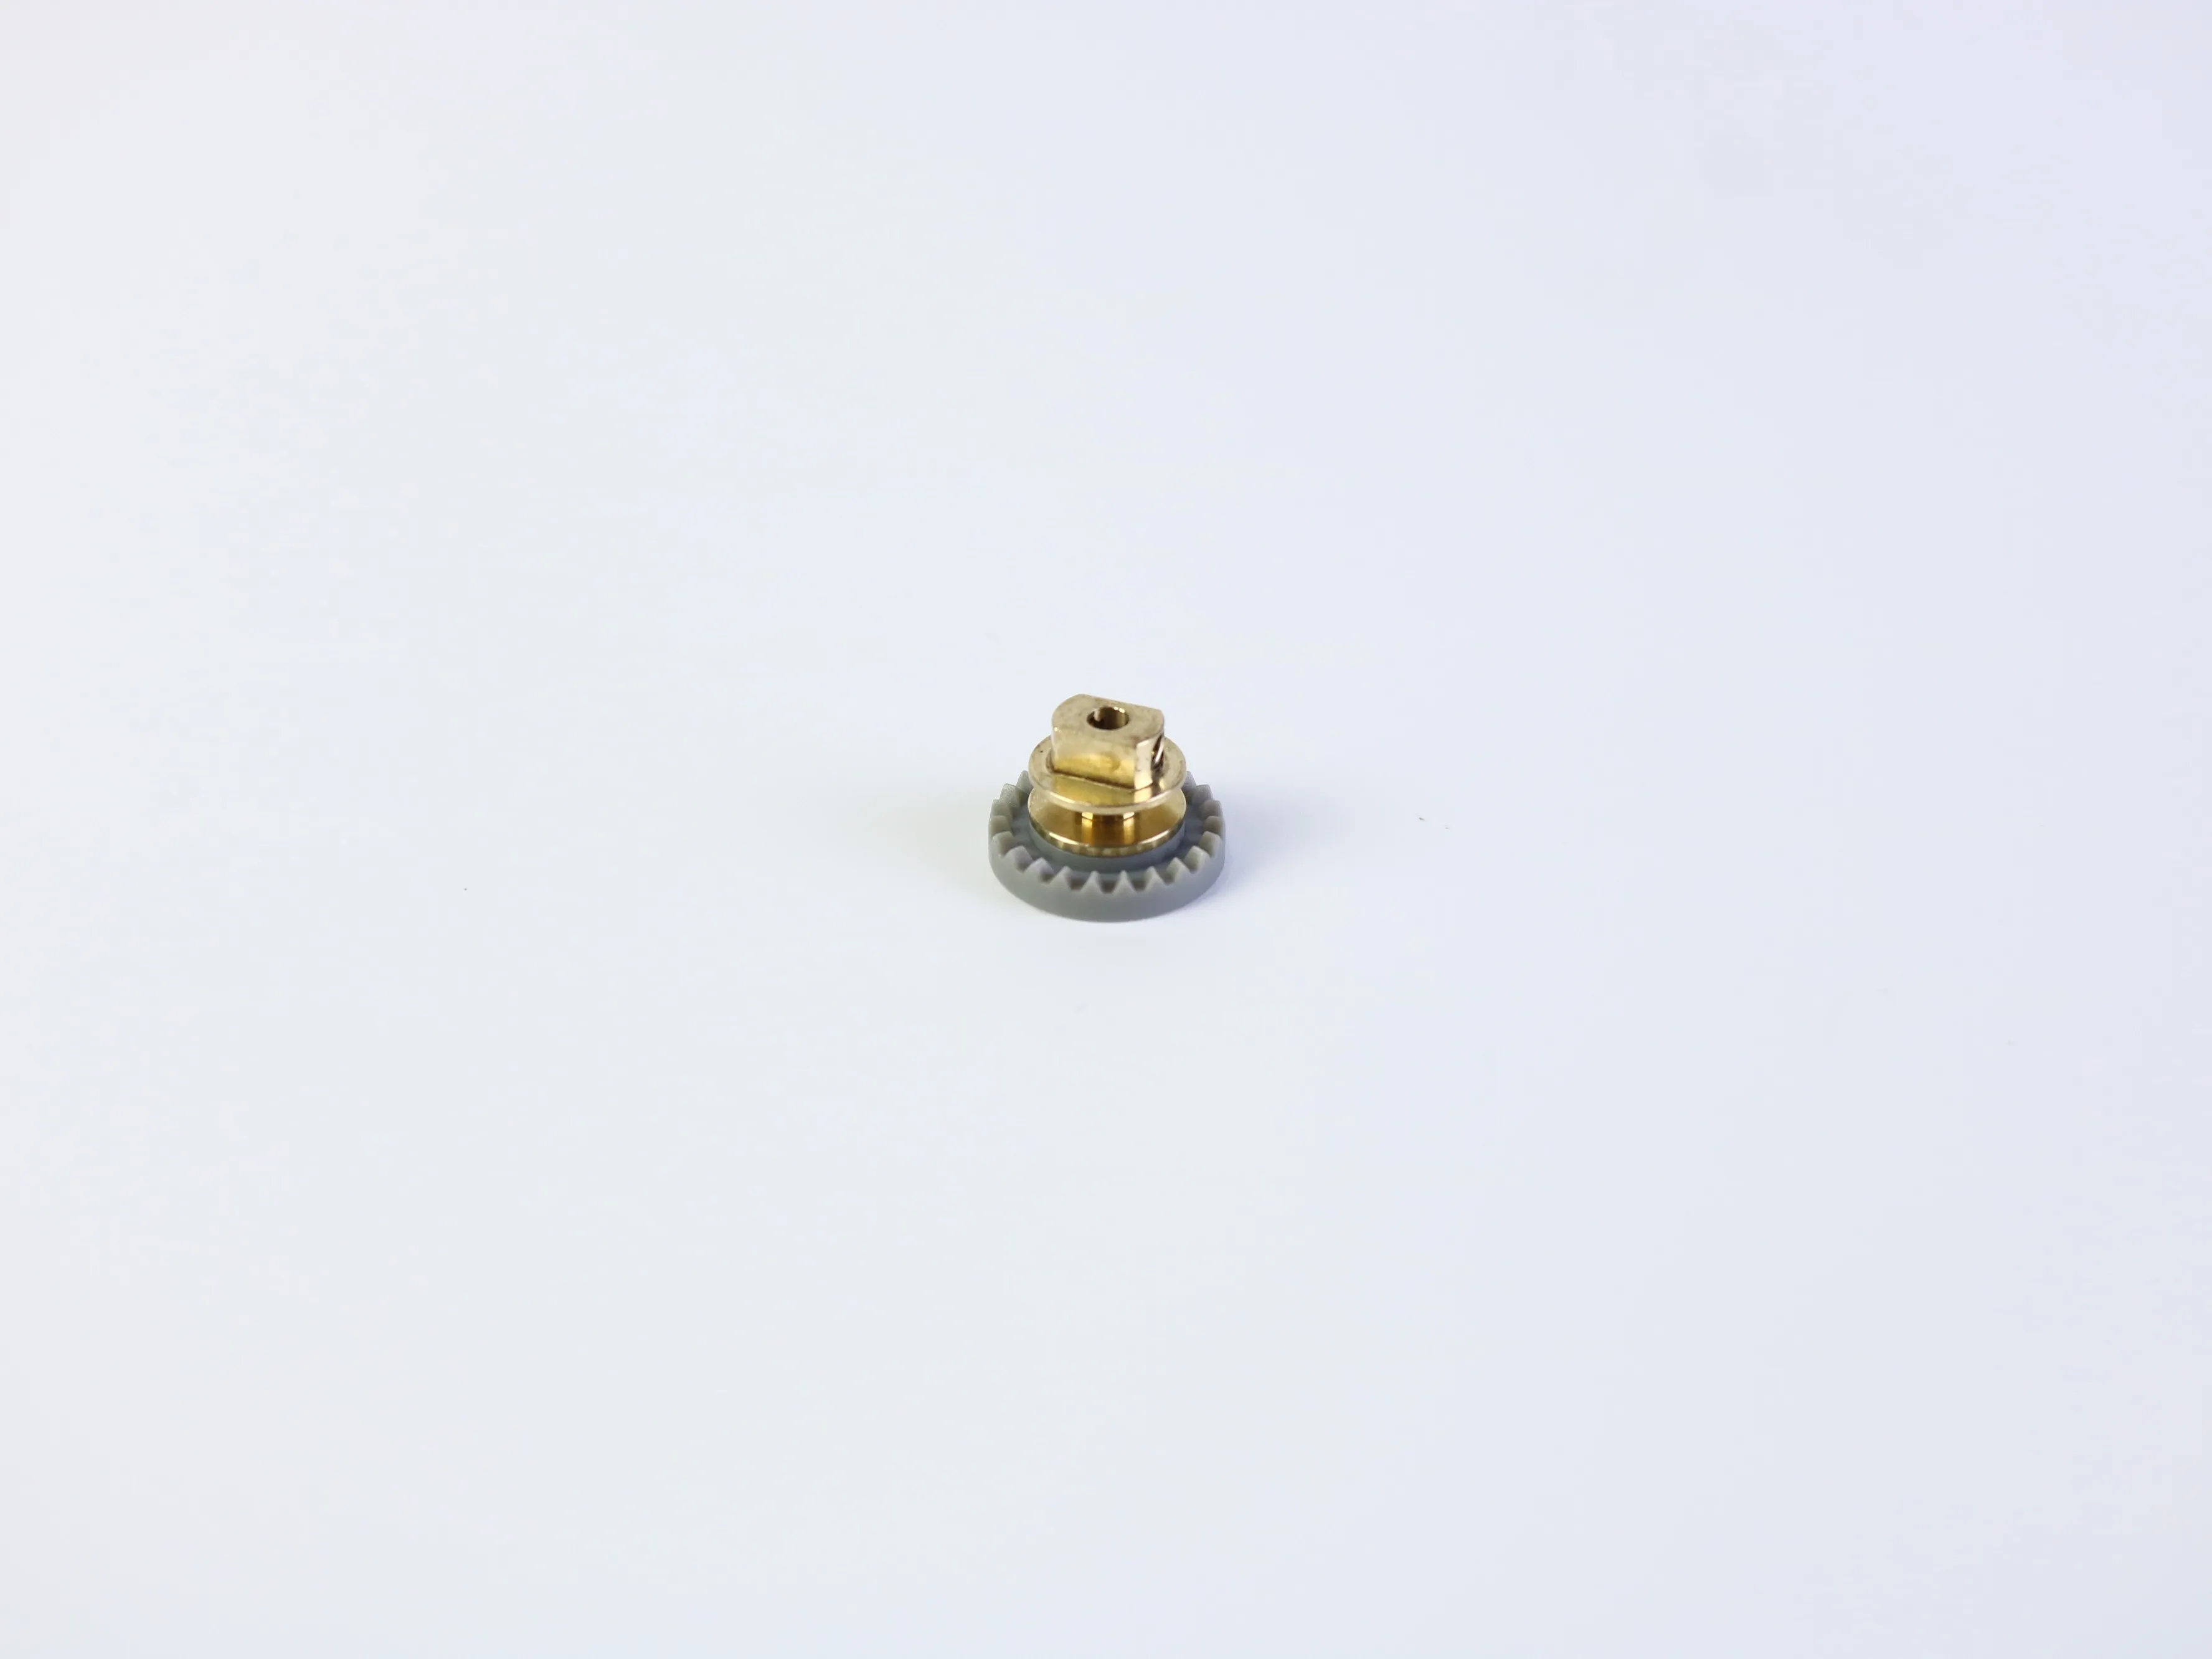
The visible part may combine several operations. A gear-and-shaft component can involve turning for the blank or shaft features, drilling or boring for the hole, milling for flats or keyways, and a dedicated gear-generating or forming process for the teeth. Secondary operations may include deburring, heat treatment, grinding, coating, cleaning, and final inspection.
The appropriate route depends on tooth form and accuracy, material and condition, quantity, integrated geometry, surface requirements, and the difference between prototype and production. A prototype route may prioritize flexibility, while production may justify dedicated tooling and more repeatable process control. Ask the supplier to explain the main cost and risk drivers. The exact toolpath or machine brand is less important than whether the proposed route is appropriate for the geometry and acceptance requirements.
5. Select material from the operating condition
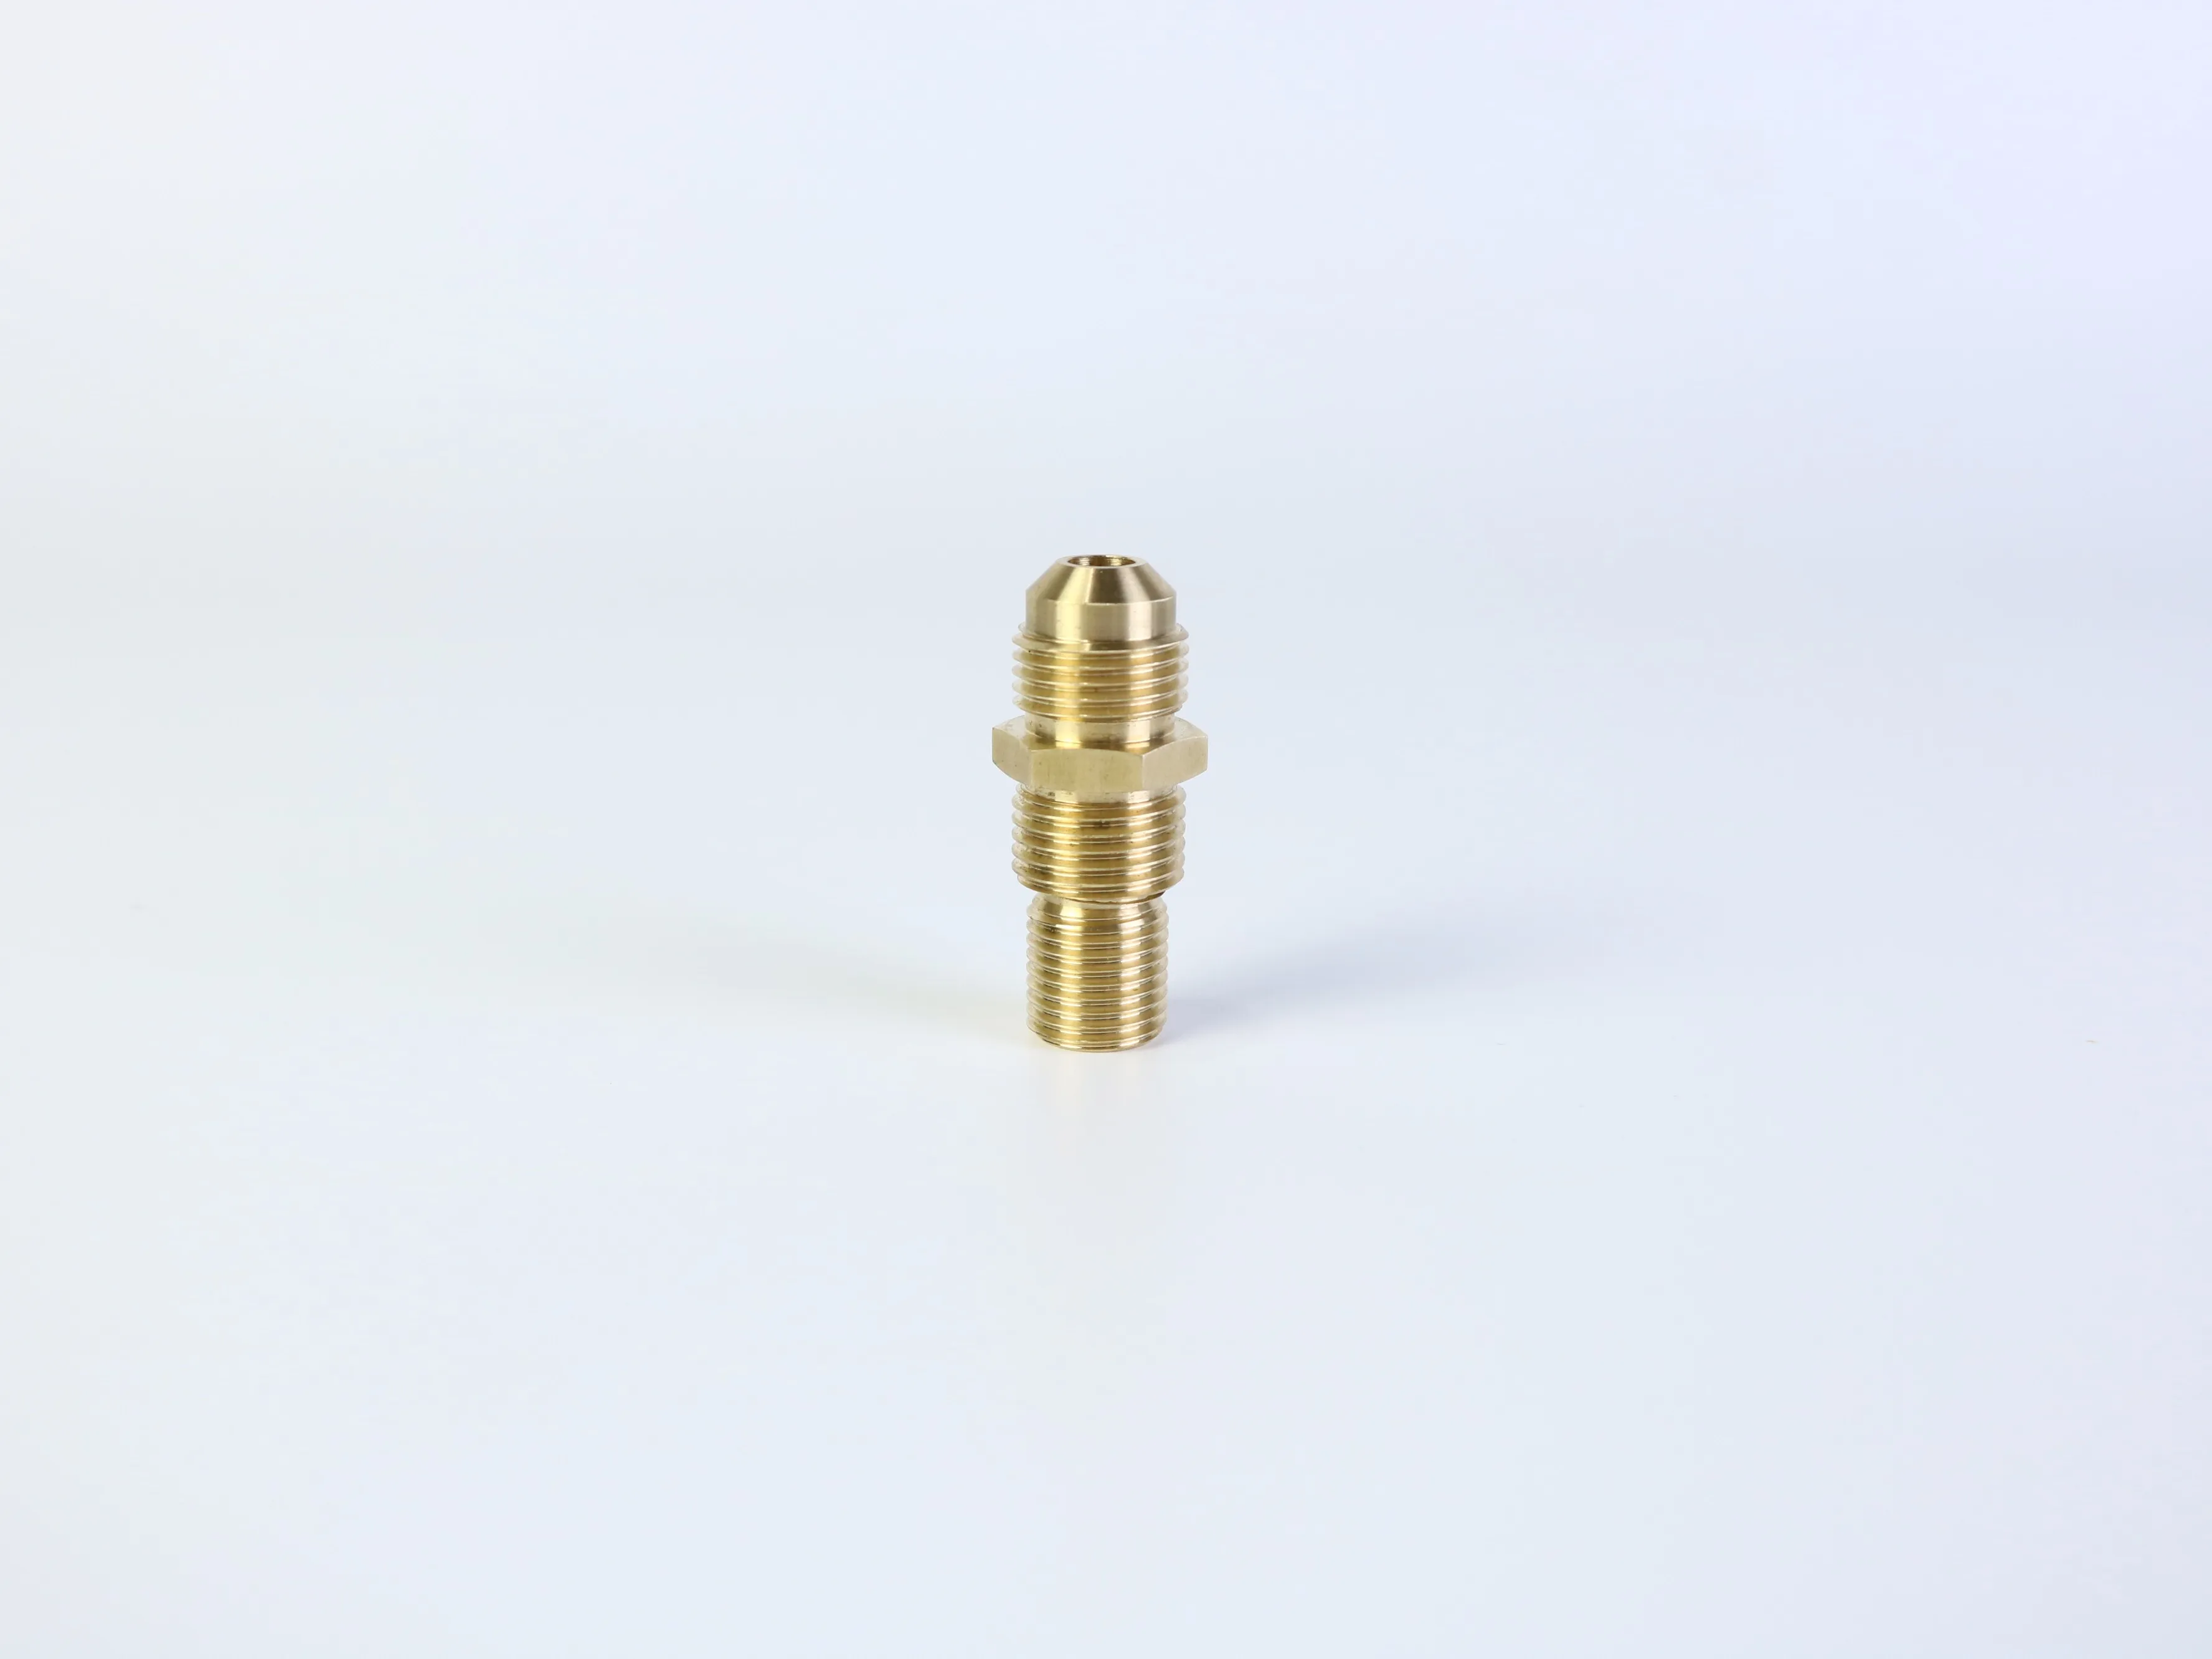
The color of a photographed part cannot verify its material grade. A brass-colored component may be brass, plated steel, coated material, or another alloy. Specify the material by recognized grade and condition, with a material certificate requirement when necessary.
Consider torque, speed, duty cycle, wear resistance, corrosion resistance, machinability, moisture, chemicals, temperature changes, contamination, heat treatment, coating, the dissimilar mating gear, weight, electrical conductivity, cleanliness, and noise. Do not select a material only because it is easy to machine. The mating pair, lubrication, load, environment, and required service life may lead to a different decision. When the application is not fully defined, request a conditional recommendation and document the assumptions behind it.
6. Build inspection into the RFQ
Inspection should be defined before production starts. The RFQ should identify the evidence required and the features that must be measured. A practical plan may include material identification, dimensional inspection of the bore, shaft, shoulders, face width, and mounting features, plus runout or concentricity checks relative to the defined datum.
Where required by the gear specification, include tooth thickness, profile, lead, pitch, or composite checks; surface roughness measurement; visual inspection for burrs, tool marks, damage, and unacceptable edge conditions; first-article or sample approval; a sampling plan; and a nonconformance procedure. The measurement method must match the requirement. A caliper may be suitable for a non-critical reference dimension, but it cannot replace a defined gear inspection method for tooth flank accuracy or backlash. Ask the supplier to identify the equipment and report format before approving the quotation.
7. Compare quotations on technical completeness
A low unit price is not necessarily a lower total cost. Review whether each quotation is based on the same assumptions. A technically responsible supplier will identify missing parameters, connect drawing requirements to process controls, and explain how conformity will be demonstrated.
- Confirm material grade and condition, heat treatment, coating, deburring, and packaging scope.
- Check that the proposed process matches the tooth form and accuracy requirement.
- Separate prototype, pilot, and production pricing.
- Make tooling, programming, setup, and one-time engineering charges visible.
- Confirm whether inspection reports and material certificates are included.
- Link delivery timing to drawing approval, material availability, and inspection requirements.
- Review any deviation from the drawing and require approval for alternatives.
- Assess whether the supplier can support a technical review before production.
Common mistakes that create gear project risk
Sending only a photo
A photo is useful for initial discussion, but it cannot define tooth geometry, fit, or acceptance criteria. Use it as a visual reference and provide a drawing, sample, or measurement plan for quotation.
Using one generic tolerance everywhere
A single general tolerance can hide the dimensions that control function. Identify critical datums, fits, runout, tooth requirements, and backlash separately.
Requesting material by appearance
Color and surface reflectivity are not reliable material identification methods. Specify the grade and certification requirement.
Requesting zero backlash without an operating definition
Backlash must be related to a mating gear, center distance, operating condition, and measurement method. Otherwise, suppliers may interpret the requirement differently.
Comparing incomplete quotations
Two prices are not comparable if one includes heat treatment and inspection while the other excludes them. Normalize the scope before selecting a supplier.
A practical RFQ checklist for custom CNC gears
Before sending the request, confirm that the package includes the following:
- Drawing revision and 3D model.
- Gear type, module or diametral pitch, tooth count, and pressure angle.
- Helix information, if applicable.
- Mating gear or center-distance information.
- Bore, keyway, shaft, and mounting requirements.
- Material grade and condition.
- Heat treatment and surface treatment requirements.
- Critical tolerances, datums, runout, and surface finish.
- Backlash or tooth-thickness requirement and measurement method.
- Quantity by prototype, pilot, and production stage.
- Inspection report and material certificate requirements.
- Packaging, marking, sample approval, and change-control expectations.
This checklist reduces quotation ambiguity without forcing the buyer to specify details that are not yet known. Unknown items can be marked for engineering review.
Frequently asked questions
Can a CNC machine shop manufacture a gear from a photograph?
What is the most important gear tolerance?
Does a tighter tolerance always make a gear better?
What files should I send with a custom gear inquiry?
Make the RFQ a shared engineering document
Custom CNC gear manufacturing becomes easier to quote and control when the RFQ describes the complete functional chain: tooth geometry, mating relationship, interfaces, material, process expectations, and inspection evidence. The goal is not to prescribe every manufacturing detail before speaking with a supplier. It is to prevent different suppliers from quoting different interpretations of the same part.
For related precision mechanical parts, review customized precision mechanical parts and CNC machining parts. For a technical review and quotation discussion, visit Request a quotation and technical review.
Table of Contents
- What should a custom CNC gear RFQ include?
- 1. Define gear geometry before discussing machining
- 2. Specify backlash as a functional requirement
- 3. Separate critical tolerances from general dimensions
- 4. Choose the manufacturing route from geometry and quantity
- 5. Select material from the operating condition
- 6. Build inspection into the RFQ
- 7. Compare quotations on technical completeness
- Common mistakes that create gear project risk
- A practical RFQ checklist for custom CNC gears
- Frequently asked questions
- Make the RFQ a shared engineering document